Need a Technical Advice?

3-Ton Copper-Zinc-Free VRC: Custom German Battery Plant Lift

Project Overview

This project was developed for an electric vehicle battery material manufacturing facility in Erfurt, Germany. The system was designed to support vertical transport of bulk material pallets between different production levels within the plant while meeting strict operational and material compatibility requirements common in battery manufacturing environments.

The application required continuous lifting of palletized ton-bag materials weighing up to 3,000 kg from the ground-level receiving area to upper-floor processing zones through a 12-meter lifting height. The lift system was configured with a multi-level loading arrangement to support efficient material flow between different production stages.

Because battery material production environments require strict contamination control and operational safety standards, the equipment was designed with specialized material selection and protective configurations suitable for sensitive industrial processing applications.

The project also required a pitless installation layout due to site construction restrictions. To support smooth pallet transfer without floor excavation, the system was designed with a low-profile loading configuration and an anti-slip loading ramp suitable for standard pallet jack operation.

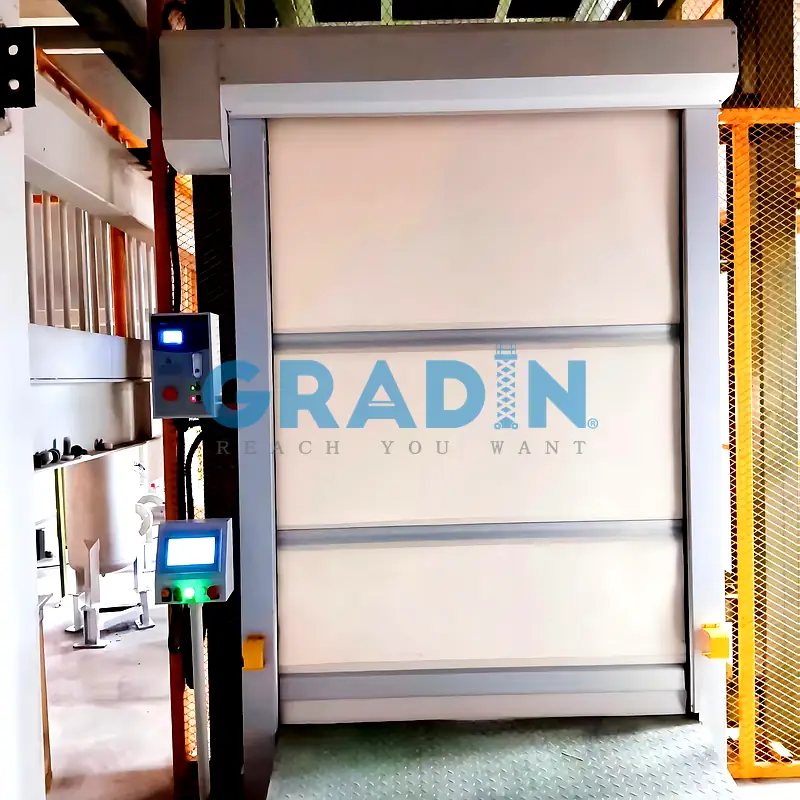
For operational safety, the lift structure was fully enclosed with industrial safety guarding and integrated rapid doors to improve personnel protection and controlled material transfer during daily production operation.

Challenge & Solution

Challenge

Before the installation of the VRC system, the battery material facility faced several operational and installation challenges related to contamination control, material transfer efficiency, and multi-floor logistics coordination.

Material Compatibility Requirements

Because the plant handles sensitive battery material products, the customer required strict control over material compatibility throughout the lifting system. Standard industrial components and conventional protective materials were not suitable for the application environment, requiring careful selection of structural and protective materials for long-term production use.

Pitless Installation with Manual Pallet Handling

Due to building structure limitations and site installation requirements, the lift system had to be installed without a floor pit. This created additional challenges for pallet transfer using standard manual pallet jacks, requiring the loading area and transfer interface to be optimized for smooth material handling at floor level.

Multi-Level Material Transfer Coordination

The facility required material transfer between multiple floors with different loading and unloading directions. To support stable automated operation, the control system and transfer sequence were configured to coordinate the different conveyor flow layouts throughout the production process.

Structural Stability During Heavy Load Transfer

The system was designed to transport palletized loads weighing up to 3,000 kg across a 12-meter lifting height. Maintaining stable lift movement and accurate floor-level positioning during frequent operation required reinforcement of the lift structure, guide system, and braking configuration.

Compliance with Industrial Safety Requirements

Because the equipment operates within a highly regulated industrial environment, the project required multiple operational safety and protection measures during system design and installation. The lift system was configured with industrial safety protection and monitoring functions suitable for continuous heavy-duty operation in European manufacturing facilities.

Solution

To meet the operational, material compatibility, and safety requirements of the battery material facility, the project was engineered as a customized vertical reciprocating conveyor (VRC) system designed for clean industrial material handling and continuous heavy-duty operation.

Material Compatibility and Protective Surface Treatment

Because the system operates in a sensitive battery material production environment, the equipment structure and exposed components were designed with special material compatibility considerations. Protective industrial coating systems and corrosion-resistant materials were selected to reduce contamination risks and support long-term operational reliability.

The lift cabin and conveyor transfer sections utilized corrosion-resistant materials suitable for clean industrial material handling environments, while sealed and low-maintenance components were used throughout the system to improve durability during continuous operation.

Pitless Installation and Pallet Transfer Configuration

The project required a pitless installation layout due to site construction restrictions. To support smooth pallet handling without floor excavation, the system was installed directly on the existing floor structure and equipped with a reinforced loading ramp configuration suitable for manual pallet jack operation.

This design allowed operators to transfer heavy palletized materials onto the platform more efficiently while maintaining safe loading conditions at ground level.

Automated Control and Conveyor Coordination

The VRC system was integrated with automated conveyor transfer stations across multiple production levels. The centralized control system coordinated lift travel, conveyor operation, and multi-level material transfer throughout the production process.

Sensor monitoring and automated transfer coordination were integrated to improve material flow stability and support reliable automated operation under continuous industrial duty cycles.

Precision Leveling and Stable Material Transfer

To improve pallet transfer stability between the lift platform and floor conveyor systems, the leveling and positioning configuration was optimized to maintain stable alignment during loading and unloading operations across the full lifting height.

This configuration helped improve transfer consistency and reduce interruption during automated pallet movement.

Safety Protection and Operational Reliability

The VRC system was equipped with multiple industrial safety protection systems suitable for continuous heavy-duty operation in a regulated manufacturing environment.

Mechanical safety protection, electrical monitoring systems, and interlocked safety doors were integrated to improve operational safety, equipment protection, and long-term system reliability during daily production use.

Technical Specifications

Parameter Specification
System Type Heavy-Duty Chain-Driven Vertical Reciprocating Conveyor (VRC)
Rated Load Capacity 3,000 kg
Vertical Travel Height 12,000 mm
Lifting Speed Variable Frequency Drive (VFD) Controlled
Conveyor Transfer Speed Continuous Automated Transfer Operation
Power Configuration AC 380V / 50Hz
Platform Size 1,500 mm × 1,500 mm × 2,100 mm
Lift Shaft Size 2,800 mm × 2,700 mm
Overall Lift Height 16,000 mm
Transfer Configuration Multi-Level C-Z Material Transfer Layout
Stops and Levels 3 Stops / 3 Levels
Leveling System Automated Positioning and Leveling Configuration
Main Structure Reinforced Structural Steel Frame
Guide System Heavy-Duty Guide Rail Structure
Drive Configuration Industrial Roller Chain Drive System
Exterior Protection Full Safety Mesh Enclosure
Counterweight System Reinforced Counterweight Configuration
Landing Protection Industrial Rapid Doors
Control System PLC and VFD Automated Control
Safety Monitoring Photoelectric Safety Detection
Surface Treatment Industrial Protective Coating System
Electrical Protection Industrial Low-Voltage Control Components
Safety Protection Overspeed and Mechanical Safety Protection
Operator Interface Industrial Outdoor Control Station
Designed Operation Continuous Industrial Duty Cycle

Project Gallery