Need a Technical Advice?

4500 kg Explosion-Proof Autoclave Shell Tilter for Mining Hydrometallurgy | Arequipa, Peru

Project Overview

Inverting heavy asymmetrical process vessels inside volatile chemical zones demands certified explosion isolation and positive mechanical clamping. This project delivered a custom explosion-proof 90-degree upender for a hydrometallurgical processing plant in Arequipa, Peru.

The operating procedure transitions 4500 kg stepped cylindrical forgings and autoclave shells between vertical flange-bolting stations and horizontal machining beds, handling workpieces inside a solvent vapor atmosphere.

  • Country / Region: Arequipa Industrial Mining Corridor, Peru (High-altitude mineral processing zone at 2300 m elevation with ambient solvent vapors and abrasive mineral dust).

  • Client Facility: Heavy Mineral Grinding Equipment Fabrication & Chemical Hydrometallurgy Overhaul Bay.

  • Equipment Model: Custom L-Frame Explosion-Proof Stepped Cylinder Upender (Model: EPU-4500-90EX). Specialized heavy turnover machines feature in our Upenders & Tilters series.

  • Key Operating Duty: Controlled 0 to 90-degree turnover of stepped cylindrical vessels (flanged end bolted, main barrel cradled in V-saddle, 4500 kg gross payload), completing the rotation in 50 to 60 seconds with hydraulic self-locking at intermediate angles.

  • Safety & Regulatory Baseline: Electric motor drive, junction enclosures, hydraulic solenoids, and the 3-meter trailing pendant meet IECEx and ATEX Ex d IIB T4 Gb ratings with IP66 ingress protection, derated for continuous operation at 2300 m altitude per IEC 60034-1.

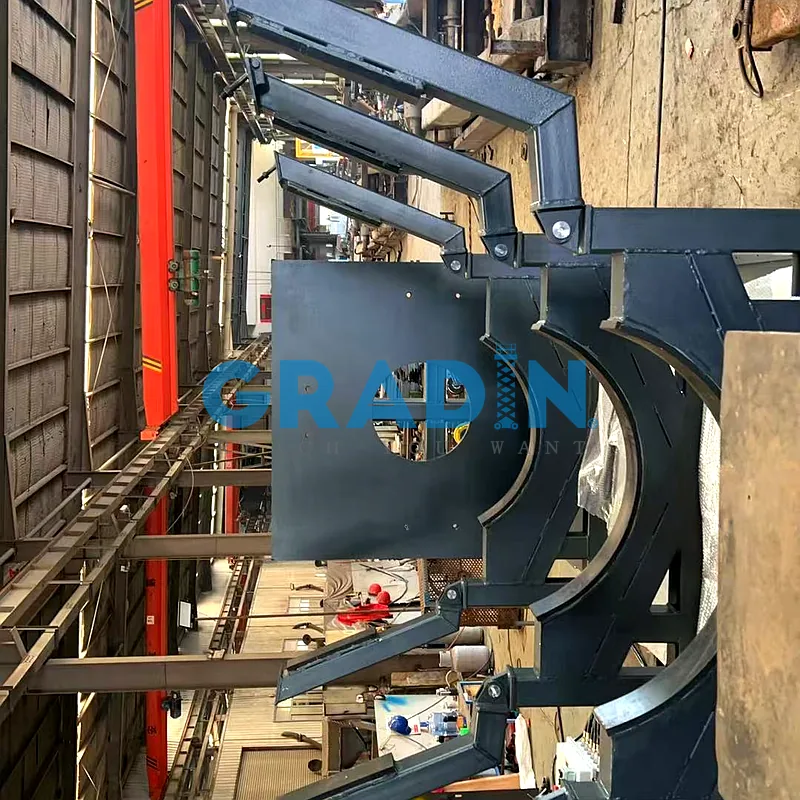
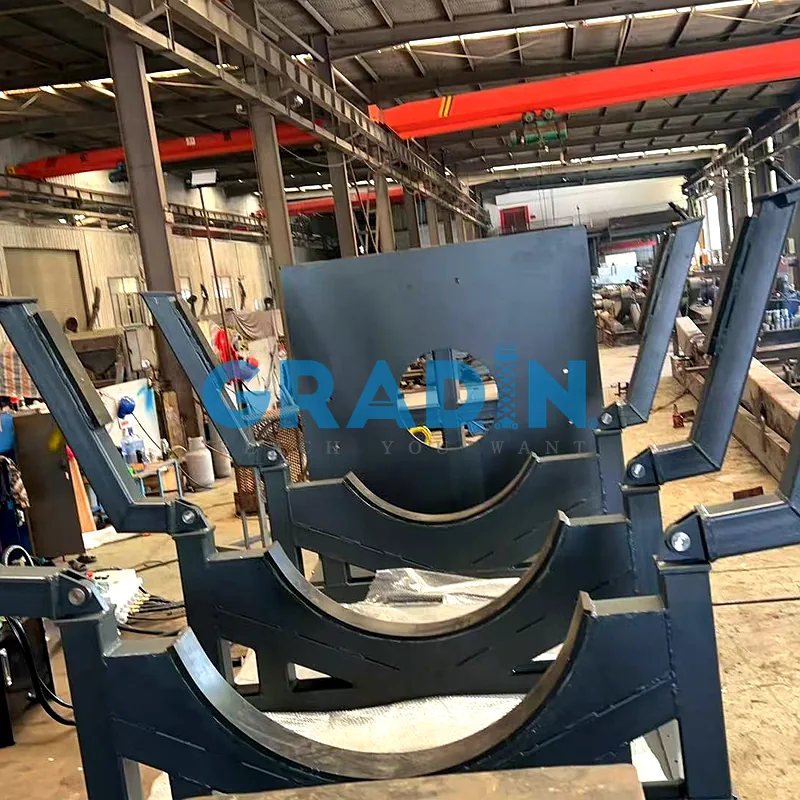
  • Structural Interface & Part Protection: L-shaped dual-table geometry combining a 2700 × 1500 mm horizontal arm with a 1500 × 1500 mm vertical platen. The 1500 mm deck incorporates CNC-machined blind-tapped holes matching the client vessel flange pattern. The 2700 mm arm features a heavy hinged V-saddle lined with 20 mm conductive anti-static ESD pads (surface resistivity under 106 Ω) to eliminate friction sparks and surface scoring on machined shells.

  • Physical Isolation & Coating: Hydraulic power pack and control cabinet sit isolated outside the splash zone, finished in marine-grade polyurethane Dark Grey RAL 7024.

Challenge & Solution

Challenge

Handling an asymmetrical stepped cylinder across a 90-degree tilt arc generates shifting torques that symmetrical coil tilters cannot manage. Deploying an explosion-proof upender for stepped mineral processing vessels requires addressing eccentric center-of-mass trajectories, barrel surface preservation, and thermal containment inside certified flameproof housings. Miscalculating gravitational overrunning loads or valve holding tolerances risks dropping 4.5 tons of equipment, shearing flange bolts, or generating incendiary sparks in a hazardous process zone.

  • Eccentric Gravitational Overrun from Asymmetrical Center-of-Gravity Shift: The workpiece pairs a small flanged end bolted to the base with an enlarged barrel cradled on the lateral arm. As the structure tilts past 45 degrees, the large-diameter barrel swings outward, driving an aggressive angular shift in the center of mass. In standard tilters using simple single-acting cylinders, this shifting weight transitions from a resisting load into an overrunning load, pulling the cylinders faster than pump fluid delivery. This fluid cavitation generates abrupt mechanical shudder, stretching base pivot hinge pins and threatening to pitch the workpiece forward off the platen.

  • Flange Bolt Shearing Combined with Barrel Scuffing Hazards: When upright, the full 4500 kg deadweight rests on the 1500 × 1500 mm platen. Between 30 and 70 degrees of tilt, the gravity vector shifts from the bottom plate to the 2700 mm lateral arm. If the hinged V-saddle clamping collar lacks sufficient radial grip, tangential sliding forces concentrate on the flange mounting bolts, snapping them in shear. Meanwhile, bare steel-on-steel clamping cuts deep bite marks and grooves into the finished vessel barrel.

  • Thermal Heat Build-Up Inside Ex d IIB T4 Flameproof Enclosures: Operating under Ex d IIB T4 explosion-proof rules mandates heavy cast-iron or thick-plate housings for the 3.0 kW pump motor, valve solenoids, and electrical switchgear. These flameproof enclosures trap internal heat. During continuous 50 to 60 second turnover sequences, hydraulic oil temperatures rise, cutting fluid viscosity. Standard directional valves begin experiencing internal spool slip, causing the platform to creep downward and lose position when held stationary at intermediate 30-degree or 60-degree crane rigging angles.

  • Crane Rigging Blind Spots and Operator Safety Clearances: Loading the 4500 kg vessel into the L-frame requires overhead bridge crane rigging. If the hydraulic power pack, electrical cabinet, and pushbuttons remain chassis-mounted on the machine frame, operators must stand inside the crushing footprint of the 90-degree tilt arc. A hydraulic line rupture or clamp failure endangers personnel, demanding physical isolation of power components and control stations outside the machine swing envelope.

Solution

Taming the shifting gravity center of an asymmetrical stepped vessel while sealing flame paths inside a volatile plant required mechanical clamping redesign and dual-circuit hydraulic locking. Engineering this explosion-proof 90-degree upender around a heavy-section L-frame, twin displacement-synchronized hydraulic rams, and an isolated explosion-proof power unit eliminated gravitational surging and barrel scratching. The structural margins, hydraulic holding tolerances, and flameproof electrical enclosures passed verified acceptance criteria during pre-shipment proof-load video testing.

  • Heavy L-Frame Geometry & Custom Tapped Mounting Platen: The core tilting frame combines a 2700 × 1500 mm horizontal arm welded from heavy structural steel channels with a perpendicular 1500 × 1500 mm base platen. The vertical 1500 mm platen is CNC-machined with a dedicated blind-tapped hole circle tailored to the client vessel flange pattern, anchoring the small-diameter neck with high-tensile M24 bolts. This positive mechanical tie absorbs 100% of the axial sliding thrust during the early stages of the 90-degree tilt, shielding the workpiece from shear slippage during 4500 kg stepped cylinder turnover.

  • Hinged V-Saddle Clamping Collar with 20 mm Conductive ESD Lining: To secure the large-diameter barrel without surface damage, the outer tip of the 2700 mm deck incorporates a heavy fabricated hinged V-saddle clamping collar. Two split clamping jaws open outward to permit direct overhead bridge crane drop-in, swinging closed under dual high-tensile clamp bolts. The curved V-saddle contact bed features a vulcanized 20 mm conductive anti-static nitrile lining (65 Shore A, surface resistivity under 

    106 Ω

     per ISO 80079-36), providing high-friction grip that stops axial creep while protecting the fine-turned autoclave shell from scratching or electrostatic spark generation.

  • Twin 90-Degree Hydraulic Tilting Cylinders with Dual Counterbalance Valves: Tilting through the 0 to 90-degree arc in 50 to 60 seconds relies on dual heavy-duty hydraulic cylinders (Ø100 mm bore / Ø70 mm rod) pinned to the lower base via forged 40Cr pivot shafts (Ø90 mm, HRC 45–50). To eliminate forward surging caused by the center-of-mass angular shift between 45 and 60 degrees, a manifold-mounted hard-seated counterbalance valve bolts to each cylinder base port. The valve maintains positive backpressure to hold the 4.5-ton load locked at any intermediate degree with under 0.1 MPa pressure drop across a 10-minute hold test, meeting ISO 4413 safety criteria.

  • Physical Component Isolation & Ex d IIB T4 Flameproof Architecture: To eliminate ignition hazards in volatile atmospheric zones, the 3.0 kW hydraulic power pack and master control console sit split-mounted 5 meters away in a protected perimeter. Electrical hardware, including the flameproof drive motor, solenoid valves, and junction boxes, carries Ex d IIB T4 ratings with IP66 ingress protection per IEC 60079-0. Internal wiring routes through steel wire raceways with serialized terminal ferrules, bonded to a continuous plant grounding busbar.

  • Dual Inching/Automatic Modes & Remote Explosion-Proof Pendant Station: Machine motion runs through a certified remote explosion-proof pendant station on a heavy 3-meter trailing armored cable, keeping the operator outside the crane rigging perimeter and tilt swing radius. The control system features a key-selectable dual mode: “Inching Mode” for millimeter-scale alignment during initial flange bolt-up, and “One-Touch Mode” for automated 90-degree continuous cycling. The panel integrates active phase-loss relays, ground-leakage interrupters, and mushroom-head emergency stop pushbuttons with yellow safety bezels.

Technical Specifications

Engineering Parameter Standard Industrial Tilter Baseline Custom Explosion-Proof Specification (Gradin) Shop Proof Verification & Compliance Standard
Equipment Model & Type Generic Hydraulic Tilter (90°) EPU-4500-90EX Stepped Cylinder Rig Serialized export unit stamped with Ex certification plate
Rated Workpiece Payload 3000 kg (Uniform symmetrical load limit) 4500 kg stepped cylinder turnover rating Proof-load tested on video at 125% rating (5625 kg)
Workpiece Geometry Envelope Standard flat pallet or symmetrical roll Stepped cylinder: small flange to large barrel Accommodates Ø500 mm to Ø1600 mm outer diameter envelope
Tilting Platform Dimensions 1800 mm L × 1500 mm W single deck 2700 × 1500 mm horizontal + 1500 × 1500 mm vertical Orthogonal heavy L-frame, deep fillet-welded steel
Small-End Vessel Attachment Flat unmachined surface, friction rest Flange platen with custom CNC blind-tapped holes M24 high-tensile bolt clamping into vessel flange face
Large-End Clamping Collar Unclamped open face (gravity resting) Fabricated hinged V-saddle clamping collar Split-jaw design with dual high-tensile clamp bolts
Contact Surface Protection Bare painted steel (scratching prone) Conductive ESD nitrile surface protection liner 20 mm vulcanized ESD bed (

Rs<106 Ω

 per ISO 80079-36)

Tilting Arc & Angular Range 0° to 90° forward tilt only 0° to 90° reciprocating continuous turnover Forward and reverse continuous cycling under full load
Turnover Cycle Duration 75 to 90 seconds (fixed speed) 50 to 60 seconds (controlled linear speed) Stop-watch timed across full 90-degree angular sweep
Hydraulic Drive Architecture Single central lift ram Dual displacement-matched hydraulic cylinders Honed ST52 steel barrels (Ø100 mm bore / Ø70 mm rod)
Overrunning Load Suppression Basic uncompensated throttle check valve Twin hard-seated counterbalance valve manifolds Eliminates surge from center-of-mass angular shift
Mid-Stroke Holding Drift Creeps 5° to 8° under thermal load Zero drift at any intermediate angle Line pressure drop 

<0.1 MPa

 across 10-minute hold

Hydraulic Power Unit Layout Chassis-mounted on tilting base External wall-mounted remote power pack skid External placement 5 meters away from volatile vapor pool
Hazardous Area Classification Non-explosion proof (unrated) Certified Ex d IIB T4 explosion-proof rating Certified compliant per IEC 60079-0 and ATEX 2014/34/EU
Enclosure Ingress Protection Standard IP54 drip-proof Sealed IP66 dust-tight and water-jet protected Tested for high-altitude outdoor and plant washdowns
Control Console & Ergonomics Frame-mounted standard pushbuttons Heavy-duty remote explosion-proof pendant station 3-meter armored trailing cable with flameproof enclosure
Operational Control Modes Single continuous run button Key-switched Dual Mode: Inching + One-Touch Auto Inching for flange bolt alignment, auto for 55s cycle
Electrical Safety Interlocks Standard thermal overload breaker Active phase-loss relay + ground-leakage breaker Integrated with dual emergency mushroom-head stop buttons
Surface Finish & Coating Single-coat synthetic alkyd primer Marine-grade epoxy anti-corrosive system, RAL 7024 Industrial dark grey finish resistant to solvent attack

Project Gallery