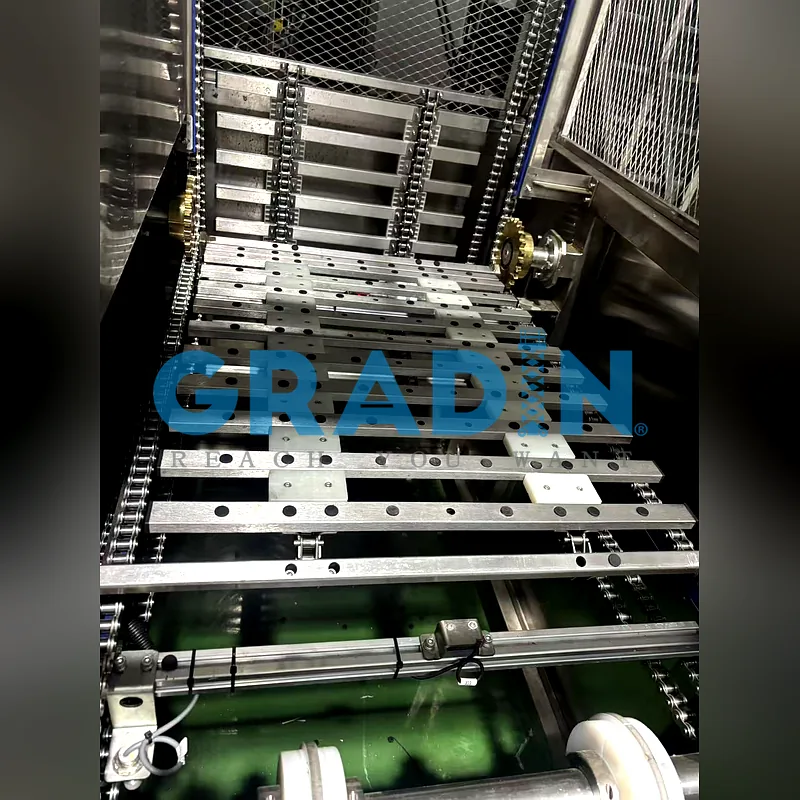
A leading infant nutrition and dairy powder manufacturing facility located in Binh Duong Province, Vietnam, required a sanitary vertical transfer system to replace an obsolete, high-maintenance reciprocating lift. The processing cleanroom elevates sealed boxes and tubs of raw milk powder ingredients (weighing up to 30 kg, with maximum dimensions of 400 mm x 600 mm x 250 mm) from a ground-level de-bagging station to an elevated 5.2-meter mezzanine blending reactor. The facility operates under strict hygienic standards, demanding zero paint flaking, zero carbon steel rust, and complete washdown compliance.
-
Country/Region: Binh Duong Province, Vietnam
-
Client Facility: Infant Formula & Nutritional Dairy Powder Cleanroom Processing Plant
-
Equipment Model: Custom Stainless Steel Z-Type Vertical Conveyor (Model: SS-ZLC-5200-SUS304)
-
Industry Classification: Food & Beverage
-
Target Material & Payload: Milk powder ingredient boxes (30 kg nominal load, dimensions <= 400 mm x 600 mm x 250 mm)
-
Continuous Elevation Rate: >= 6 units per minute (360 to 480 cartons per hour continuous throughput)
-
Overall Equipment Footprint: 1,400 mm (L) x 1,100 mm (W) x 5,200 mm (H)
-
Infeed & Outfeed Elevation: Infeed conveyor 1,000 mm above finished floor, discharge conveyor 1,000 mm above mezzanine deck
-
Installation Constraint: Restricted interior door access requiring complete Modular Knock-Down Assembly for on-site bolting
To meet strict international hygiene regulations and continuous dairy production demands, factory configured the unit as an automated Sanitary Milk Powder Elevator conforming to the ASME B20.1 Safety Standard for continuous vertical material conveyors . The structural framework features a rigid SUS304 Four-Column Frame paired with precision food-grade drive chains. Management integrated this sanitary continuous vertical lift alongside custom stainless sanitary vertical lifters to modernize their ingredient staging workflow.